Butt Fusion vs Electrofusion: Which HDPE Pipe Joining Method Fits Your Project?
- Share
- publisher
- Riyang
- Issue Time
- Aug 28,2026
Summary
Butt fusion and electrofusion both produce strong, leak-tight HDPE joints, but they suit different jobs. This guide compares how each method works, pipe size and alignment limits, fittings versus reusable tooling, surface preparation, traceability, and lifecycle cost so you can choose the right joining method for your pipeline, repair, or tie-in project.
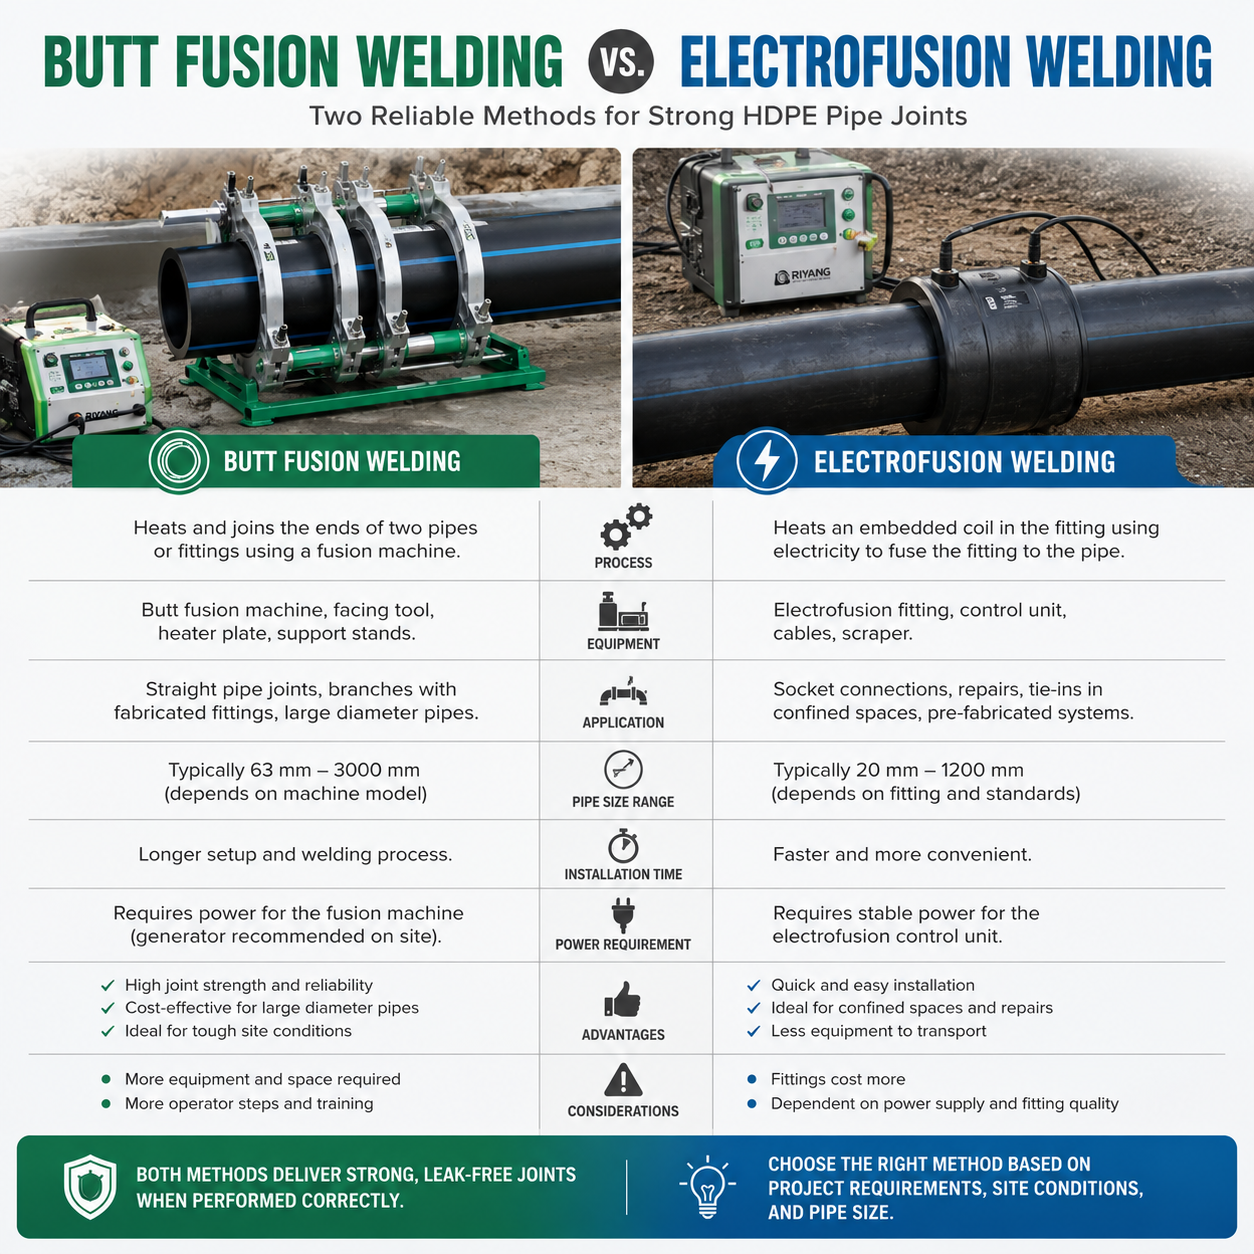
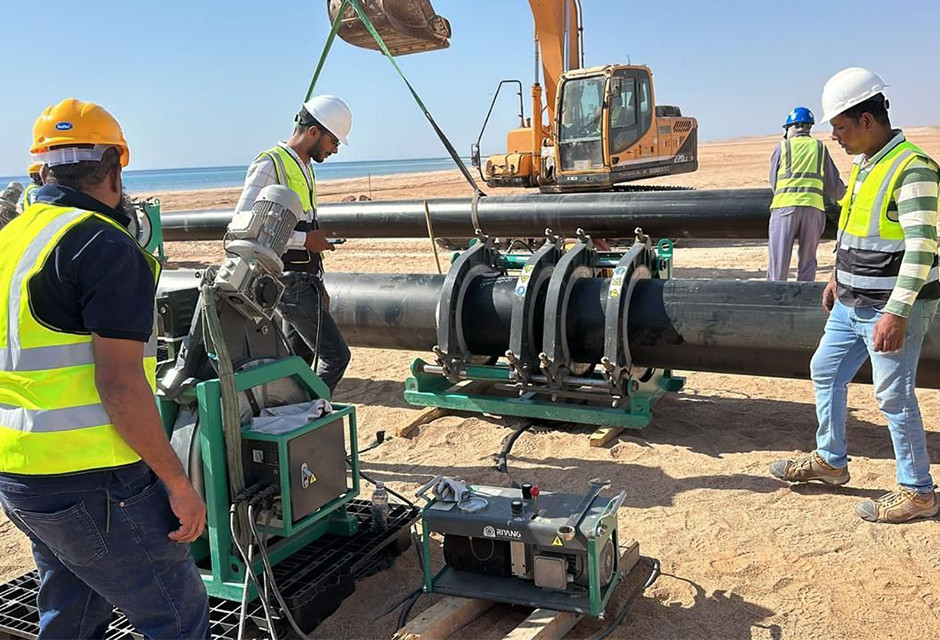
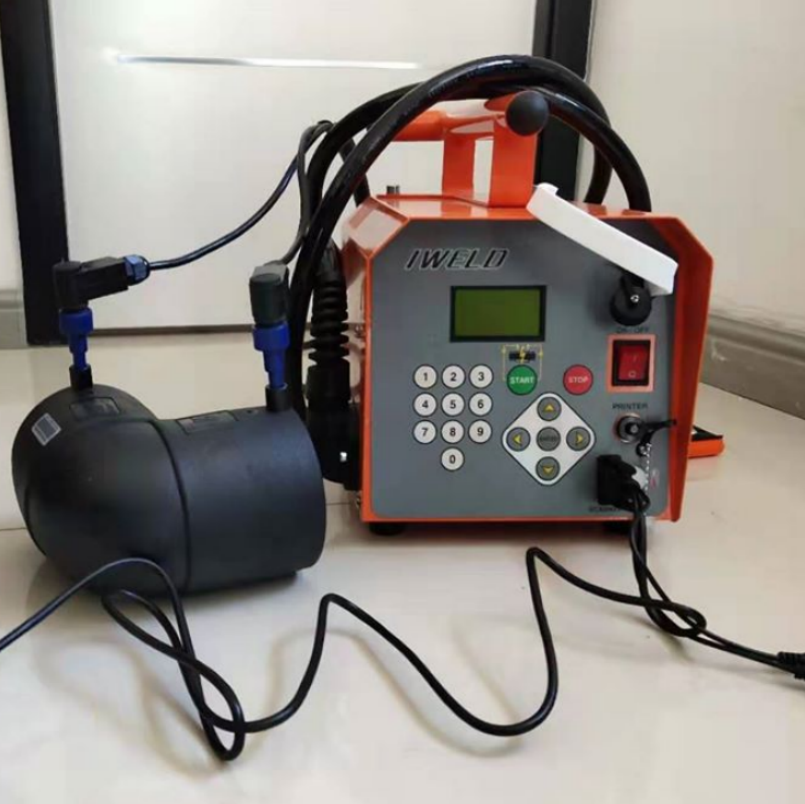
Butt fusion and electrofusion are both heat-fusion methods for joining HDPE pipe, but they suit different jobs. Butt fusion heats and presses pipe ends together directly and is the workhorse for long, straight runs of large-diameter pipe. Electrofusion uses a fitting with a built-in heating coil and is preferred for repairs, tie-ins, and tight-access work. Choose butt fusion for long straight pipelines and large diameters; choose electrofusion for restricted access, repairs, and joining different wall thicknesses or diameters. The two methods produce strong, leak-tight joints but differ in how the weld is formed and where each is most cost-effective. The table below summarizes the main practical differences. Butt fusion joins two pipe ends into a single continuous piece of polyethylene. The pipe ends are clamped in a butt fusion welding machine, faced flat with a facing tool to remove the oxidized surface and produce square, parallel faces, then pressed against a heater plate at a controlled temperature. Once the faces reach the correct molten condition, the plate is removed and the two ends are brought together under a controlled pressure and held until the joint cools. The result is a homogeneous weld with a small internal and external bead. Butt fusion requires both pipe ends to be the same material, the same nominal diameter, and the same wall thickness. The low, uniform profile of a butt joint, and the ability to remove the external bead where required, make the method well suited to trenchless installation techniques such as sliplining, pipe bursting, and directional drilling. Electrofusion uses a fitting that contains a resistive heating coil embedded near its inner surface. The prepared pipe ends are inserted into the fitting, and an electrofusion welding machine passes a controlled electric current through the coil. The coil heats the surrounding polyethylene, melting the inner surface of the fitting and the outer surface of the pipe together. The joint is held in the clamps and allowed to cool under restraint before the fitting is disturbed. Because the energy is delivered inside the fitting, electrofusion is far less dependent on the skill of the operator than a manually controlled heat soak. Modern machines read the fitting barcode and apply the correct voltage and fusion time automatically, which also supports reliable data logging. For long, straight runs of new pipeline in open-cut trenching, butt fusion is usually the first choice. It produces a continuous, monolithic string of pipe with no added fitting at each joint, and the per-joint cost stays low even as the diameter grows. This is why butt fusion dominates trunk mains and large-diameter transmission lines. Electrofusion can also be used on straight runs, and it is common for smaller-diameter distribution and service lines where joints are numerous and access is limited. The trade-off is that each joint carries the cost of a consumable fitting, which can become significant across a long pipeline. Electrofusion is the preferred method when space is tight or when the work is a repair rather than a fresh installation. Couplers, repair saddles, and patch fittings let a crew join or repair pipe inside a trench, around other utilities, or against an existing live main without the long machine bed and straight alignment a butt fusion machine requires. Electrofusion is also the standard way to add a new service or branch to an existing PE main using saddle fittings and tees. Butt fusion still has a role in repairs, but it generally needs more room to position the machine and align the pipe, so it is less practical for confined, in-ditch tie-ins. The two methods place different demands on the pipe itself. Butt fusion requires the two ends to match in outside diameter and wall thickness, and the machine clamps normally correct the slight ovality that can develop during storage and transport. The pipe must also be aligned on a common axis so the joint forms evenly around the full circumference. Electrofusion is more forgiving of geometry. With suitable fittings it can join pipes of different wall thickness and, in some cases, different grades of polyethylene such as MDPE to HDPE. However, the pipe ends inserted into the socket must be round, within the tolerance stated by the fitting manufacturer. If the ends are oval beyond that tolerance, they must be re-rounded with clamps before insertion, otherwise the annulus between pipe and fitting becomes irregular and the joint can fail. One of the clearest cost differences is where the money goes. Butt fusion is tooling-intensive but consumable-light: the machine, the facing tool, and the heater plate are used across thousands of joints. Electrofusion flips this: the machine is comparatively simple, but every single joint consumes a fitting whose price climbs with diameter. On a large-diameter main, the fitting cost for electrofusion can far outweigh the machine cost of butt fusion, which is a key reason large mains are almost always butt fused. Both methods fail without clean, dry, correctly prepared pipe ends, and both should be performed by trained, qualified operators. For butt fusion, the facing step planes the ends flat and removes the oxidized surface layer before heating. For electrofusion, the pipe ends must be mechanically scraped to remove the oxide layer, to the depth specified by the fitting manufacturer, and marked to the correct insertion depth. Grease, moisture, and dirt must be kept off the prepared surface, and work should be protected from wind and weather that can cool or contaminate the weld. The exact scraping depth, heating temperature, fusion pressure, and cooling times are set by the fitting, pipe, and equipment manufacturers and by the applicable installation standard. These are not universal values; always follow the written procedure for the specific products being joined. Both methods support strong quality records, which matters for utilities and specification work. A modern butt fusion machine logs heater temperature, fusion pressure, drag pressure, fusion time, and in many cases bead dimensions, allowing each joint to be reviewed against its procedure. Electrofusion machines record voltage, current, fusion time, and the fitting barcode, tying every joint back to a specific fitting and its parameters. Some electrofusion fittings also include a visual fusion indicator that confirms the cycle was completed. These data logs support inspection and acceptance, and visual checks of the finished joint, such as bead size and shape on butt fusion, remain part of routine quality control. Butt fusion is normally the lowest total cost: reusable tooling, no per-joint fitting expense, and fast continuous production along a straight alignment. Electrofusion is often cheaper overall once restricted access and rework risk are counted, because the machine is smaller and the cycle is less operator-dependent, even though each fitting adds cost. Total cost should weigh machine capital, operator training and time, per-joint consumables, and the risk and cost of a failed joint that must be cut out and remade. The cheapest method per joint is not always the cheapest method for the project. Use the checklist below to narrow the choice quickly. Compare Riyang butt fusion and electrofusion solutions to match your pipe range, site access, and quality-recording requirements. No. Butt fusion requires both pipe ends to be the same material, the same nominal diameter, and the same wall thickness. Electrofusion can accommodate different wall thicknesses with suitable fittings. Electrofusion is usually better, because it needs far less room and no long, straight alignment. Couplers and repair fittings are designed for exactly this kind of confined, in-ditch work. Generally not. Electrofusion fittings protrude beyond the pipe surface, so they are less suited to trenchless methods. Butt fusion, with its low profile and removable external bead, is the standard choice for trenchless installation. It is most common below about 250 mm OD, largely because fitting cost rises with diameter, but there is no strict technical upper limit. In practice, large-diameter mains are almost always butt fused for cost and strength. Butt fusion typically depends more on operator judgment during heating and bead formation. Electrofusion is more machine-controlled, so the cycle is less dependent on manual skill, though both require trained operators. Yes. The oxidized surface layer must be removed by scraping, to the depth specified by the fitting manufacturer, before the pipe is inserted into the fitting. Have a specific pipe size or repair scenario in mind? Contact us to discuss which HDPE joining method fits your project.Butt Fusion vs Electrofusion at a Glance
Criterion Butt Fusion Electrofusion How the joint forms Pipe ends are heated and pressed together directly A heating coil embedded in the fitting melts the pipe and fitting together Typical pipe range Roughly 50 mm to 2000 mm OD Roughly 16 mm to 710 mm OD; most common below 315 mm Wall thickness Pipe ends must match in diameter and wall thickness Different wall thicknesses and diameters can be joined with suitable fittings Consumables No fitting needed for a straight join; tooling is reusable One consumable fitting per joint, cost rising with size Site access Needs room around the pipe and straight axial alignment Works in trenches and low-clearance spaces Operator dependence Higher; operator reads heating and bead behavior Lower; the machine controls the fusion cycle Traceability Logs temperature, pressure, time, and bead dimensions Logs voltage, current, time, and fitting barcode Trenchless methods Well suited; low profile, external bead can be removed Less suited; fittings protrude beyond the pipe surface How Butt Fusion Works
How Electrofusion Works
Straight Pipeline Installation
Repairs, Tie-Ins, and Restricted Access
Pipe Size and Alignment Requirements
Consumable Fittings vs Reusable Tooling
Operator Preparation and Surface Scraping
Traceability and Quality Controls
Lifecycle Cost by Project Type
Large-Diameter Straight Mains
Small Lines, Repairs, and Tie-Ins
Decision Matrix and Checklist
Frequently Asked Questions
Can butt fusion join pipes with different wall thicknesses?
Which method is better for a repair inside a trench?
Can electrofusion be used for directional drilling or sliplining?
Is electrofusion only for small-diameter pipe?
Which method needs more operator skill?
Do I need to scrape the pipe before electrofusion?
Key Takeaways
References